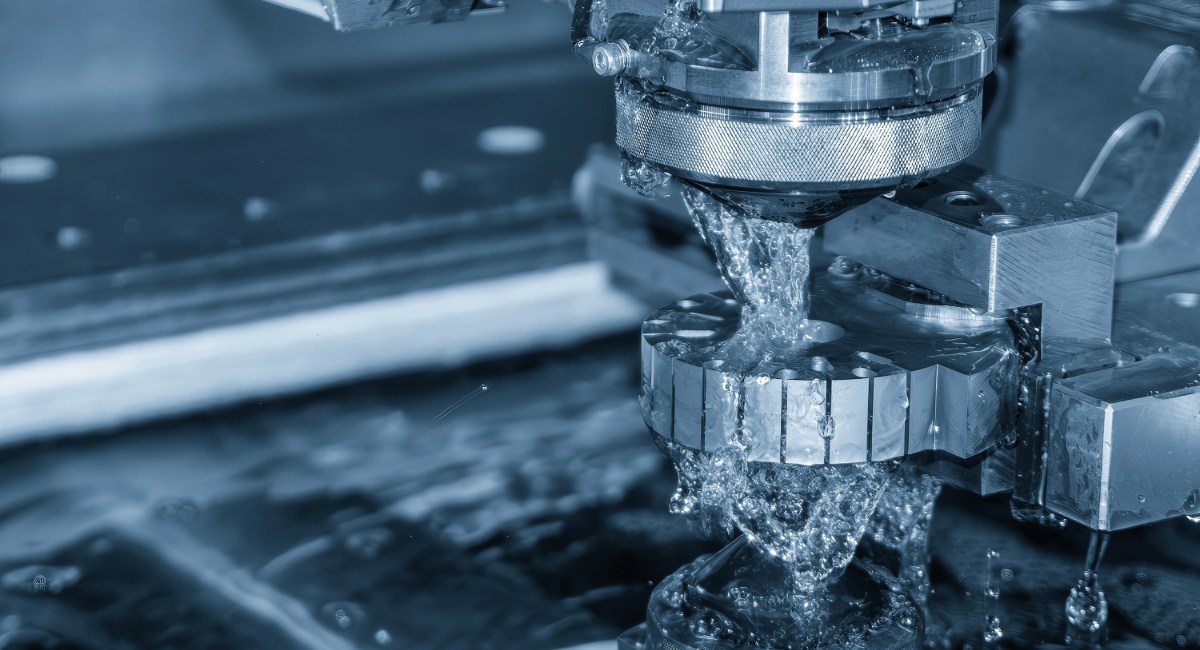
Ann Arbor, MI, wire EDM parts are conductive metal components cut or finished with wire EDM, especially when the part needs clean internal geometry, narrow slots, sharp corners, or accurate profiles.
At Roberson Machine Company, we machine wire EDM parts for tooling, replacement components, production work, and projects that require controlled features and repeatable accuracy.
Learn More About
For complex conductive-metal parts, our team can look at your print, material, tolerances, and production requirements before recommending the right path forward. Contact us online or call 573-646-3996 to discuss wire EDM parts in Ann Arbor, MI, and other precision CNC machining services.
What Types of Parts Are Made With Wire EDM?
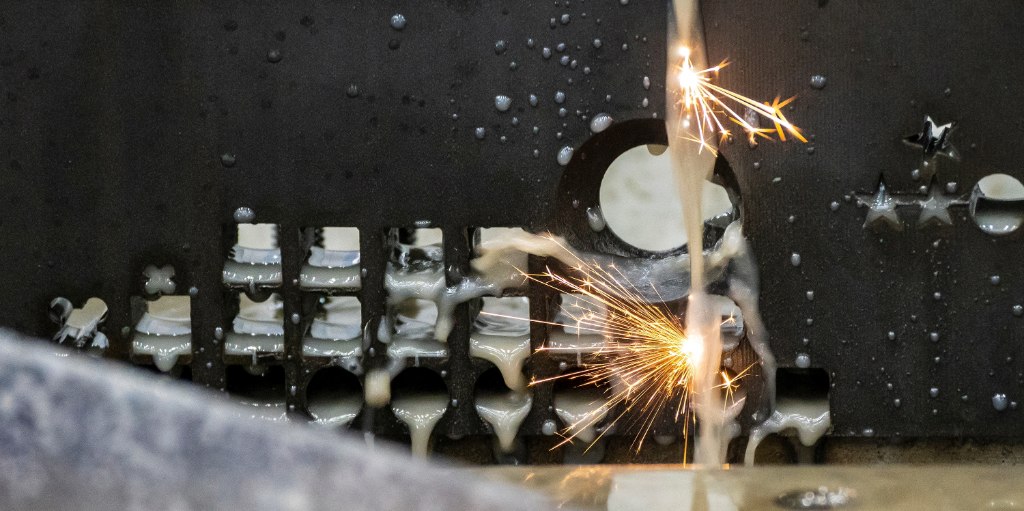
Wire EDM is used with conductive metals when the finished part needs clean through-cuts, controlled internal geometry, narrow openings, or accurate profiles that conventional cutting tools cannot produce as efficiently. The process is often used for customer parts where one critical feature controls how the component fits, moves, wears, or repeats in production.
Where Wire EDM Fits in Part Production
Wire EDM is often used for tooling, production support, replacement work, and parts where one critical feature controls performance. It can produce precise profiles, internal cutouts, narrow slots, insert openings, fixture details, and inspection features that standard cutting tools may not handle as cleanly. Common examples include:
- Repeat-production tooling: Production tooling used for stamping, forming, cutting, and repeat manufacturing work where edge quality, profile control, and wear performance matter.
- Mold inserts: Tooling inserts often use wire EDM when the part needs a controlled profile, fine internal detail, or wear surface that supports repeat production.
- Machining fixtures and gauges: Fixtures and gauges may need controlled slots, profiles, or locating features that support repeatable machining, inspection, or assembly.
- Instrument parts: Instrument parts may use wire EDM when the design includes fine openings, small profiles, or geometry that needs to stay consistent.
- Sealing and flow-control features: Flow-control parts may need clean slots, internal openings, or controlled profiles that affect movement, sealing, or performance.
- Recreated components: Hard-to-source parts may need wire EDM when the replacement must match the original geometry closely enough to fit and function.
- Splined and keyed parts: Parts where keyways, slots, splines, internal profiles, fit, or clearance control the finished function.
- Carbide and hardened parts: Components that need clean cutting, accurate profile work, or low-force machining after heat treat or material preparation.
When Should Wire EDM Be Used for Ann Arbor, MI, Parts?
Wire EDM machining becomes useful when a conductive material and a difficult feature come together. If conventional tools cannot cut the profile, slot, opening, or internal geometry cleanly, wire EDM may be the better path.
Feature geometry through the full thickness
Wire EDM can help when a feature needs to hold its shape through the full material thickness, not just from one side of the part.
- Through-cut profiles, internal openings, and shaped features
- Narrow slots, keyed features, and slotted components
- Gauges, dies, tooling inserts, and profile-critical components
Cutting challenges inside the part
Some features create machining problems because they are too narrow, too deep, too hard, or too delicate for a conventional cutting approach.
- Thin sections, sharp inside corners, and fine details
- Hardened parts that need profile work after heat treat
- Small openings or details with limited tool access
Small details with a large effect
Not every wire EDM part is complex from end to end. Sometimes one slot, opening, profile, keyway, die detail, or clearance feature determines whether the component fits, locates, moves, seals, wears, or repeats correctly in production.
From Print to Production for Ann Arbor, MI, Wire EDM Parts
A wire EDM part usually starts with a review of what the print actually requires. Material, quantity, tolerances, model data, and critical features all affect whether wire EDM for parts and projects should carry the main cut, handle one detail, or fit into a larger production plan.
- Start with the drawing or sample: Send whatever part information is available, from drawings and CAD files to material needs, quantities, samples, and critical feature notes.
- Review the critical features: The team looks for the details that decide whether wire EDM is needed, such as internal geometry, keyway features, cutouts, hardened areas, or repeat-production fit requirements.
- Confirm how the part should be made: Some parts may be cut primarily with wire EDM, while others may need milling, turning, heat treat, or other work before EDM finishes the critical feature.
- Machine the part and confirm the result: After the process plan is confirmed, the part is machined and inspected against the print, assembly needs, and production requirements.
- Build a cleaner repeat process: Recurring wire EDM parts can benefit from saved part information, process history, and clear notes about the features that matter most.
For manufacturers, the finished component needs to meet the drawing, fit the assembly or tooling process, and remain repeatable for future production needs.
Repeat Wire EDM Parts for Ann Arbor, MI, Manufacturers
Wire EDM is not limited to one-off problem parts. It can support production runs, recurring orders, and components that need to return to the same geometry across future releases. That matters when a part has a slot, profile, opening, insert detail, or inspection feature that needs to stay consistent from run to run.
Wire EDM can support bulk part production with CNC machining when one EDM feature needs to repeat cleanly across the order. Other production steps may prepare, shape, or verify the part while wire EDM handles the cut that needs controlled geometry or low-force machining.
- Repeatable feature geometry: Profiles, slots, cutouts, keyways, and other feature-critical details can stay consistent across repeat orders.
- Repeat-order scheduling: Production teams can plan repeat work more cleanly when material needs, quantity changes, and inspection requirements are understood before scheduling.
- Machining paths that stay predictable: A stable route can combine CNC milling for high-volume production parts with wire EDM when the surrounding geometry and EDM feature both need control.
For repeat work, Roberson Machine Company can review quantities, release timing, material needs, and critical features before the wire EDM process is planned around both current and future orders.
Where Ann Arbor, MI, Wire EDM Parts Are Used
Wire EDM parts support industries that rely on wire EDM when one feature affects fit, motion, inspection, repeatability, or production performance.
- Aerospace: Wire EDM can help produce aerospace components where controlled profiles, shaped openings, or difficult conductive materials are part of the job.
- Medical: Medical work may involve instrument components, surgical tooling, medical valve bodies, and small conductive parts that need clean feature geometry.
- Automotive and EV: Powertrain tooling, mold inserts, keyed features, and production support parts with fine internal clearances.
- Packaging: Packaging equipment may need wire EDM for forming tools, wear components, cutting details, and repeat-production tooling.
- Automation and robotics: Fixtures, gauges, end-of-arm tooling details, housings, and motion-critical components with controlled internal features.
- Oil and energy: Pump components, sealing features, replacement parts, and hardened alloy details may need wire EDM when service conditions make geometry and material performance important.
Materials for Wire EDM Parts in Ann Arbor, MI
Wire EDM requires conductive material, but the best material still depends on how the finished part will be used. The decision may involve wear life, corrosion resistance, weight, conductivity, heat treatment, inspection needs, and later production steps.
Production parts with repeated contact
Tool steels carbides, and hardened steels are often selected for components that see repeated production contact, cutting edges, forming pressure, or locating work. Common examples include:
- Production punches and dies
- Insert tooling
- Hardened wear plates
- Hardened production details
Wire EDM is useful here because critical profiles can often be cut after the material has been hardened.
Parts that need corrosion resistance
Stainless steel and other corrosion-resistant alloys are commonly used when parts face moisture, cleaning requirements, food production, medical environments, or similar service conditions. Wire EDM can support clean internal features where tool access would otherwise limit the cut.
Conductive metal components
Aluminum, brass, copper, and other conductive metals can support components that need:
- Lower weight for housings, brackets, or production support components
- Electrical or thermal conductivity
- Clean openings, shaped slots, or accurate profiles tied to the part’s function
The process can help when conductive parts need controlled feature geometry without relying only on conventional tool access.
Post-heat-treat feature work
The challenge is not always the full part. Sometimes the problem is one feature that needs to be finished after heat treat, inside a hard section, or in a tight area. Wire EDM can handle that feature without changing the entire production plan.
Which CNC Machining Methods Pair With Wire EDM?
Ann Arbor, MI, wire EDM part may need EDM for one critical feature and another CNC machining method for the surrounding geometry. That split can help match the process to the part instead of forcing one method to do everything.
- CNC milling: Used to prepare or finish part geometry around the EDM work, including flats, pockets, drilled features, and mounting surfaces.
- CNC turning: Used when the component needs round features, turned surfaces, bores, grooves, or shoulders as part of the finished geometry.
- 5-axis machining: Used when complex geometry, angled details, or multi-face features need to be machined around the EDM work.
- Multi-axis machining: Used when the part needs multiple sides or angles machined without adding unnecessary setup changes.
Roberson Machine Company can review the print, material, features, and production needs to determine where wire EDM fits in the process.
Frequently Asked Questions About Ann Arbor, MI, Wire EDM Parts
Customers often ask whether wire EDM is the right fit, what details help with quoting, and how the process works alongside other machining steps. These FAQs cover wire EDM parts, materials, production planning, replacement work, and cost factors.
What information helps quote wire EDM parts in Ann Arbor, MI?
The more part context you can provide, the easier it is to quote accurately. Drawings, CAD files, samples, material details, thickness, tolerances, quantity, timing, and inspection needs all help.
Helpful details to send include:
- Prints, models, or sample parts
- Material requirements and stock thickness
- Fit-critical dimensions and feature callouts
- Run quantity and expected repeat demand
- Any inspection, finish, or documentation needs
If the quote details are still developing, an early review can still help identify whether wire EDM should carry the main cut or finish one critical feature.
What materials are common for Ann Arbor, MI, wire EDM parts?
Wire EDM requires electrically conductive material. Common choices include stainless steel, aluminum, brass, copper, titanium, tool steels, carbides, and hardened steels.
The part’s use should drive the material choice. A wear-focused part, tooling insert, stainless component, lightweight housing, or conductive detail may each require a different material before EDM cutting begins.
Can wire EDM be one step in a larger machining process?
Wire EDM is often part of a larger machining route. Other CNC processes may create the surrounding geometry, while EDM handles the slot, profile, opening, or internal detail that needs more control.
In a larger process, wire EDM is used where it adds the most value: feature control, clean cutting, and access that other tools may not provide.
When does wire EDM make sense for repeat production?
Wire EDM can support recurring orders when the critical geometry has to stay consistent. That may include profiles, slots, inserts, fixture details, gauge features, replacement parts, and production tooling components.
Repeat work usually benefits from stable drawings, defined material requirements, known inspection needs, and consistent release quantities. Those details help keep the machining path more predictable when the job returns.
Is wire EDM useful for recreating replacement parts?
Wire EDM can support new production parts, replacement components, and tooling details when a critical feature needs accurate geometry. For replacement work, that may mean recreating a worn or obsolete feature from a print, model, or sample.
Replacement work is easier to review when the original part information is available. Samples, old drawings, material notes, wear patterns, and assembly requirements can help define the finished part’s job.
What drives wire EDM part cost and timing?
Cost and timing usually come down to material, thickness, tolerances, feature complexity, inspection needs, and the number of steps required to finish the part. A simple profile in prepared stock is very different from a hardened component with EDM features, inspection needs, and other machining requirements.
Timing and cost often depend on:
- Material type, hardness, and thickness
- Number of profiles, openings, slots, or internal features
- Dimensional requirements, finish needs, and critical feature control
- How the part needs to be held, set up, and inspected
- Quantity, repeat demand, and delivery timing
Clear requirements up front make it easier to quote the job accurately and choose the right machining path.
Partner With Roberson Machine Company for Ann Arbor, MI, Wire EDM Parts
Roberson Machine Company works with customers who need controlled profiles, clean internal features, repeatable accuracy, and a practical path from print to finished part.
EDM support within the machining process
Our team can review the full part requirement, including whether EDM should work alongside milling, turning, 5-axis machining, multi-axis machining, inspection, or other production steps.
Consistency across repeat part runs
Machined parts often need to come back the same way across future runs, replacement needs, or larger production schedules. Roberson Machine Company works with parts where controlled geometry, reliable feature quality, and repeatable output matter over time.
Review from prints, models, or samples
Bring the part details you have, including drawings, models, samples, material requirements, quantities, tolerances, or future production needs. We can review the information and help plan the machining route.
Related machining services include:
- Automated CNC Milling Machine
- Plastic Machining
- Laser Engraving
- Lathe Machine
- Precision Stainless Steel Machining
- CNC Lathe Machining
- Custom CNC Machining for Part Production
- CNC Machine Automation
- Oil and Gas Precision Machining
Roberson Machine Company can help review wire EDM parts that need controlled profiles, clean internal features, and a practical path from print to production. Learn more about how wire EDM can help your business, contact us online, or call 573-646-3996 to discuss Ann Arbor, MI, wire EDM parts for your next project.